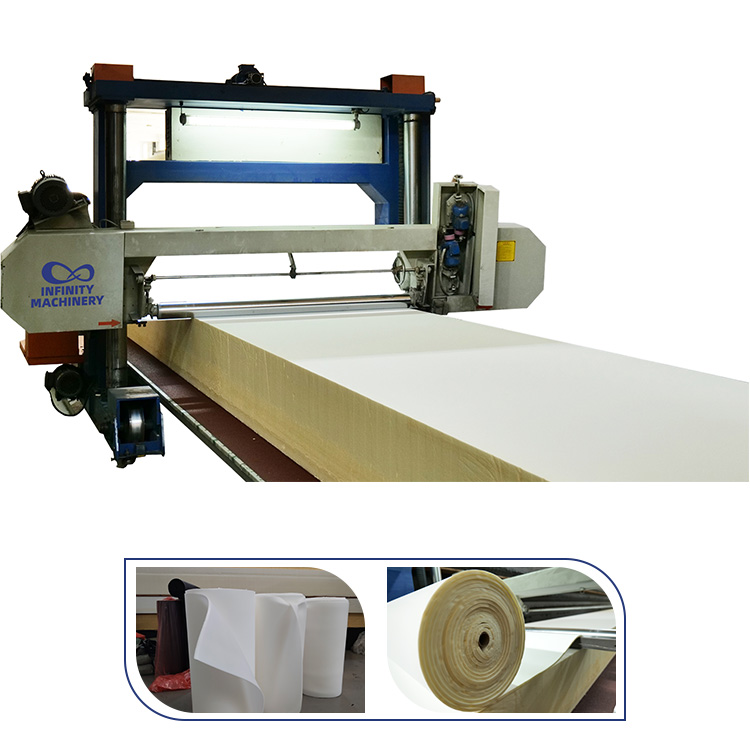
The foam cutting department is the dust factory of the mattress plant: the horizontal cutter, the contour cutter and the boring machine shave the foam into the fine particles, and the fine foam dust floats in the air, settles on the surfaces and clings to the fresh quilted covers with the static charge. The dust that lands on the fresh cover is not a cosmetic speck, it is a reject: the dark dust particle on the white cover, the static-cling dust on the fabric, and the cover that must be re-cleaned, re-quilted or scrapped before it reaches the border line. The dust extractor is the machine that captures the dust at the source, before it floats, settles and stains, and the extraction setup decides whether the cutting room is the dust factory or the clean room. The IF-LT1650/2450 Horizontal Long Track Foam Cutting Machine, the IF-YX01/YX02 Profile Sponge Cutting Machine and the IF-Z01 Foam Boring Machine are the machine cases this guide maps. This guide explains the static dust problem, the staining mechanism, the extraction setup and the clean-room habits that keep the fresh covers clean.
The dust problem starts with the physics of the foam cutting: the horizontal blade shaves the foam block into the sheets, the contour cutter profiles the shapes and the boring machine drills the holes, and every cut releases the fine foam particles into the air. The foam dust is light, dry and charged: the cutting friction builds the static charge on the particles, and the charged dust floats instead of falling, drifts across the room with the air movement and clings to the first surface it touches. The fresh quilted covers are the perfect landing surface: the fabric is clean, white and freshly opened, the static charge of the fabric attracts the charged dust, and the dark particle on the white cover is immediately visible. The dust that lands on the cover is the reject chain: the cover is sent back for the re-cleaning, the re-quilting or the scrap, the border line waits for the replacement panel, and the dust speck that cost a fraction of a cent to create costs the fabric, the labor and the line time to remove. The cutting room without the extraction is the dust factory that feeds the whole plant, and the dust extractor is the first line of defense that captures the particles at the source.
The dust is generated at every cutting station, and the extraction captures it at each source before it joins the air, the surfaces and the fresh covers.
The staining mechanism explains why the dust is not just the dirt but the specific enemy of the fresh cover, and the mechanism has three parts. Part one is the particle size: the foam cutting dust is the fine fraction, the particles below the half millimeter that stay suspended in the air for the minutes instead of falling in the seconds, and the suspended dust is the dust that travels. Part two is the static charge: the cutting friction charges both the dust and the fabric, the charged dust is attracted to the charged fabric surface, and the attraction is strongest on the dry synthetic cover fabrics that the mattress plants use, so the fresh cover pulls the dust out of the air. Part three is the visibility: the foam dust on the white quilted cover is the dark speck that the customer sees at the first glance, and the speck on the border fabric, the handle or the quilting line is the reject trigger, because the mattress is sold on the clean first impression. The staining mechanism is the reason the dust control is not the housekeeping nicety but the quality gate: the factory that controls the dust protects the covers from the first cut to the final pack, and the factory that ignores the dust pays the rejects at the border line.
Particle size: foam cutting dust below 0.5mm stays suspended for minutes and travels | Static charge: cutting friction charges dust and fabric, the charged dust is attracted to the dry synthetic covers | Visibility: the dark speck on the white quilted cover is the reject trigger at first glance | The staining mechanism makes dust control a quality gate, not housekeeping
The extraction setup is the engineering answer, and the principle is simple: capture the dust where it is created, not where it lands. The setup has the extraction point at every cutting station: the horizontal cutter draws the slice dust through the hood at the blade, the contour cutter pulls the shape shavings through the profile head, and the boring machine captures the drill dust at the bore point, so the dust goes into the duct before it floats. The duct network carries the captured dust to the central collector, the cyclone or the bag filter, and the collector separates the dust from the air and returns the cleaned air to the room. The extraction capacity is sized to the cutting room: the airflow is measured in the cubic meters per hour, and the rule is the extraction at the source with the hoods close to the cut, the duct velocity that keeps the dust moving and the filter that handles the cutting room volume. The machine integration matters: the extraction is built into the cutting machine design, with the hood at the blade and the duct connection ready, so the extraction is the part of the cutting process, not the afterthought, and the operators run the extraction with the machine, not as the occasional clean-up. The extraction setup is the difference between the dust factory and the clean room, and the setup is measured by the dust that never reaches the air.
The air quality math turns the dust control into the investment decision, and the numbers are simple. The reject cost without the extraction: the cutting room that runs without the extraction sends the dust onto the fresh covers, the cover rejects climb to the two percent or more of the quilted panels, and each rejected panel costs the fabric, the quilting labor and the replacement cycle, often two to three times the panel value by the time the border line waits. The extraction cost: the dust extractor and the duct network for the cutting room is the one-time investment with the modest running cost, the filter maintenance and the power, and the extraction captures the ninety percent or more of the dust at the source. The comparison: the factory that rejects the two percent of the quilted panels pays the reject cost every day, and the extractor that cuts the rejects to the fraction of the percent pays for itself in the months. The air quality math also counts the softer savings: the machines run cleaner with the less dust in the bearings and the electronics, the operators breathe the cleaner air with the less respiratory exposure, and the cutting room is the safer and the more pleasant workplace. The extractor is the machine that pays back on the rejects it prevents, and the air quality math is the justification that the owner understands.
The reject math is the first number, and the cleaner machines and the healthier operators are the second, and the two together justify the extraction for every cutting room.
The extractor is the machine, and the clean-room habits are the discipline that makes the machine work. Habit one is the separation: the cutting room is separated from the quilting and the cover handling, with the door and the air pressure that keeps the cutting dust out of the clean area, so the fresh covers are opened and quilted in the dust-free zone. Habit two is the surface discipline: the cutting tables, the machines and the floors are wiped and vacuumed at the shift end, so the settled dust is removed before it is re-suspended by the next shift. Habit three is the cover handling: the fresh fabric rolls stay wrapped until the quilting, the opened panels are covered or moved promptly, and the covers never sit in the cutting room air. Habit four is the maintenance schedule: the filters are cleaned and replaced on the schedule, the ducts are checked for the blockages and the hoods are adjusted to the cut, because the extractor that runs with the clogged filter is the extractor that does not extract. The clean-room habits are the daily complement to the extraction machine, and the factory that runs the habits with the extractor keeps the covers clean from the first cut to the final pack.
Separation: cutting room separated from quilting and cover handling, door and air pressure keep the dust out | Surface discipline: tables, machines and floors wiped and vacuumed at shift end | Cover handling: fresh rolls stay wrapped, opened panels covered or moved promptly | Maintenance: filters cleaned and replaced on schedule, ducts checked, hoods adjusted
The implementation plan builds the dust-free cutting room in five steps, run at the line. Step 1: the dust map, walking the cutting room and marking every dust source, the horizontal cutter, the contour cutter, the boring machine and the transfer points, and measuring the dust that settles on the test covers. Step 2: the extraction sizing, calculating the room volume, the number of cutting stations and the required airflow, and selecting the extractor and the duct layout that covers the sources. Step 3: the installation, mounting the hoods at the cutting stations, running the ducts to the central collector and commissioning the extraction with the test cuts. Step 4: the clean-room habits, introducing the separation door, the shift-end cleaning and the cover-handling rules, and training the operators to run the extraction with the machine. Step 5: the re-measure, running the extraction for a month, re-counting the cover rejects and the dust on the test covers, and comparing against the dust map baseline; the falling rejects prove the extraction, and the clean covers prove the clean room. The factory that runs the five steps gets the cutting room that cuts the foam without the dust on the covers, and the fresh panels that reach the border line clean.
The IF-LT1650/2450, the IF-YX01/YX02 and the IF-Z01 are the cutting and boring machines with the extraction points this guide maps, and the five-step plan builds the dust-free cutting room in your factory. Contact our foam team for the dust map for your cutting department, the extraction sizing and the clean-room setup that keeps your fresh covers clean.
Contact our foam team today for the dust control setup for your cutting department: the dust map, the extraction sizing, the hood and duct configuration and the clean-room habits that keep your fresh covers clean from the first cut to the final pack.