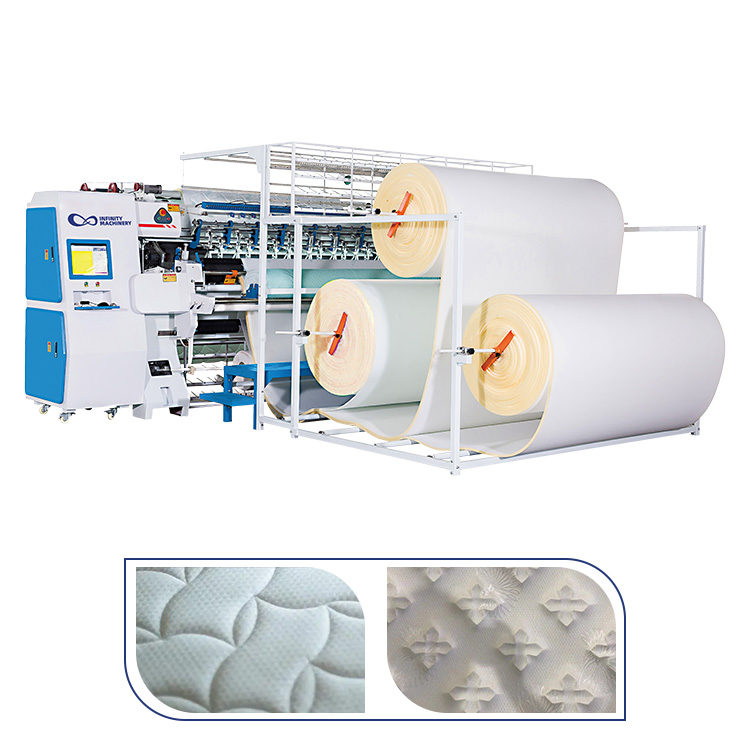
The factory hall question is a math problem before it is a machinery problem, and the 1000m2 hall fits a full mattress line when the footprint is planned. The usable footprint is the first number: the gross 1000m2 loses the columns, the walls, the offices, the toilets and the walkways, and the usable production floor typically lands the 750-800m2, so the layout starts from the usable number, not the gross. The zone map is the second: the hall splits into the raw material store, the foam and spring lines, the quilting and sewing, the assembly, the packing and the finished goods buffer, and each zone gets the footprint that matches its throughput. The machine footprint is the third: the IF-Q-1200 Multi-Functional Quilting Machine, the IF-FF3 Automatic Box Foaming Machine and the IF-CR8 Compression and Roll Packing Machine each carry a known footprint, an operating clearance and a service margin, and the sum of the machine footprints plus the aisles and the buffers decides the fit. The flow rule is the straight line: the material enters at one end and the finished roll exits at the other.
The factory layout starts from the usable footprint, and the gross 1000m2 is not the number the machines see. The gross area is the first number: the 1000m2 measured to the outer walls, and the gross is what the building brochure quotes. The deductions are the second: the structural columns (each column carries a 0.5-1.5m clearance the machine cannot use), the wall clearance (the 0.5-1m perimeter margin), the offices and the toilets and the fire escapes, and the sum of the deductions lands the usable floor. The usable footprint is the third number: the 1000m2 gross with the 15-25 percent deduction leaves the 750-800m2 of usable production floor, and the layout that plans from the usable number fits the line while the layout that plans from the gross runs out of room. The footprint rule: draw the gross rectangle, mark the columns, the walls and the fixed rooms, subtract the clearances and only then place the first machine.
The zone map divides the hall into six zones, and the allocation follows the material flow instead of the convenience. The raw material store is the first zone: the foam blocks, the fabric rolls, the wire coils and the adhesive drums sit at the receiving end, and the store carries the 7-14 days of material with the racks that stack the volume. The foam and spring zone is the second: the foaming machine and the spring lines sit near the raw store, the foaming needs the ventilation and the height, and the springs feed the core assembly. The quilting and sewing zone is the third: the quilting machines, the panel cutter and the hemming machines sit in the middle on a clean, flat floor, and the quilting output feeds the assembly. The assembly zone is the fourth: the core, the comfort layers and the cover come together on the assembly stations, and the assembled unit moves to the packing. The packing zone is the fifth: the compression, the roll packing and the case packing sit at the shipping end, with the machine clearance and the dispatch staging. The finished goods buffer is the sixth: the packed rolls stage before the truck, the buffer holds the 2-3 days of output and the buffer sits at the dock. The zone rule is the flow rule: each zone hands its output to the next in a straight line.
The machine footprint is the sum that decides the fit, and each machine carries three numbers: the footprint, the clearance and the service margin. The footprint is the machine base: the length and the width that the machine body occupies on the floor, and the IF-Q-1200 Multi-Functional Quilting Machine carries its quilting head and table, the IF-FF3 Automatic Box Foaming Machine carries its box and the pump skid and the IF-CR8 Compression and Roll Packing Machine carries its press and the roll station. The clearance is the operating ring: the 0.8-1.5m around the machine for the operator, the material feed and the output take-away, and the clearance doubles the perceived footprint of the machine. The service margin is the access: the 0.6-1m behind and the side for the maintenance, the panel opening and the parts pull, and the margin keeps the machine serviceable without the tear-down. The sum math: the three machines with their footprints, clearances and margins occupy a meaningful band of the hall, and the layout that places the line with the clearance and the margin on the plan fits the line while the layout that packs the machines tight fails the service. The footprint rule: list every machine with its footprint, clearance and margin before the layout.
The aisle and the flow design is where the hall either fits or fights, and the straight line is the layout that wastes the least floor. The main aisle is the first: the 2.5-3m main aisle runs the length of the hall and carries the forklift, the trolley and the material, and the main aisle is the spine of the flow. The cross aisles are the second: the 1.5-2m cross aisles connect the zones and let the operator move without walking the length of the hall, and the cross aisles break the long runs into the short trips. The workstation aisles are the third: the 0.8-1.2m aisles around the workstations and the machines keep the operator room without the wasted floor, and the workstation aisle matches the reach of the operator. The flow rule is the one-way rule: the material moves one way from the receiving to the shipping, the operators move along the aisles and the returned empty pallets move on the opposite path.
The buffer and the inventory space is the floor that the layout often forgets, and the hall that skips the buffer overflows into the aisles and the machines. The raw material buffer is the first: the 7-14 days of foam, fabric and wire sit at the receiving end, and the raw buffer needs the racks and the lanes that hold the volume off the floor. The work-in-process buffer is the second: the quilted panels, the assembled cores and the packed units sit between the stations, the WIP buffer absorbs the speed difference between the fast machines and the slow stations, and the WIP sits in the lanes beside the line. The finished goods buffer is the third: the packed rolls stage before the truck, the finished buffer holds the 2-3 days of output and the buffer needs the space at the dock. The spare parts and the maintenance area is the fourth: the lubricants, the spare parts and the tool bench sit in the corner, keeping the spares off the production floor. The buffer rule is the 10-15 percent rule: the layout that reserves the 10-15 percent of the usable floor for the buffers and the inventory fits the full line, while the layout that gives the whole floor to the machines runs out of the staging space and the flow stalls.
The fit path turns the hall into the plan in the six steps, and the steps follow the math instead of the guess. Step one is the measure: the factory measures the gross hall, marks the columns, the walls and the fixed rooms and computes the usable footprint. Step two is the zone map: the factory assigns the six zones to the usable floor and marks the receiving and the shipping doors on the plan. Step three is the machine footprint: the factory lists every machine with its footprint, clearance and service margin and places the machines in their zones with the clearance on the plan. Step four is the aisles: the factory draws the main, the cross and the workstation aisles and checks that the material moves one way from the receiving to the shipping. Step five is the buffers: the factory reserves the 10-15 percent for the raw, the WIP and the finished buffers and confirms the staging lanes are on the plan. Step six is the check: the factory walks the plan, measures the machine-to-machine and the aisle gaps and adjusts the tight spots before the concrete is poured. The fit rule: the plan that fits the usable floor with the zones, the machine footprints, the aisles and the buffers on the drawing fits the real line.
Contact our team for the factory floor plan template, the machine footprint data and the quilting, foaming and packing machines that fit your hall with the measured layout.